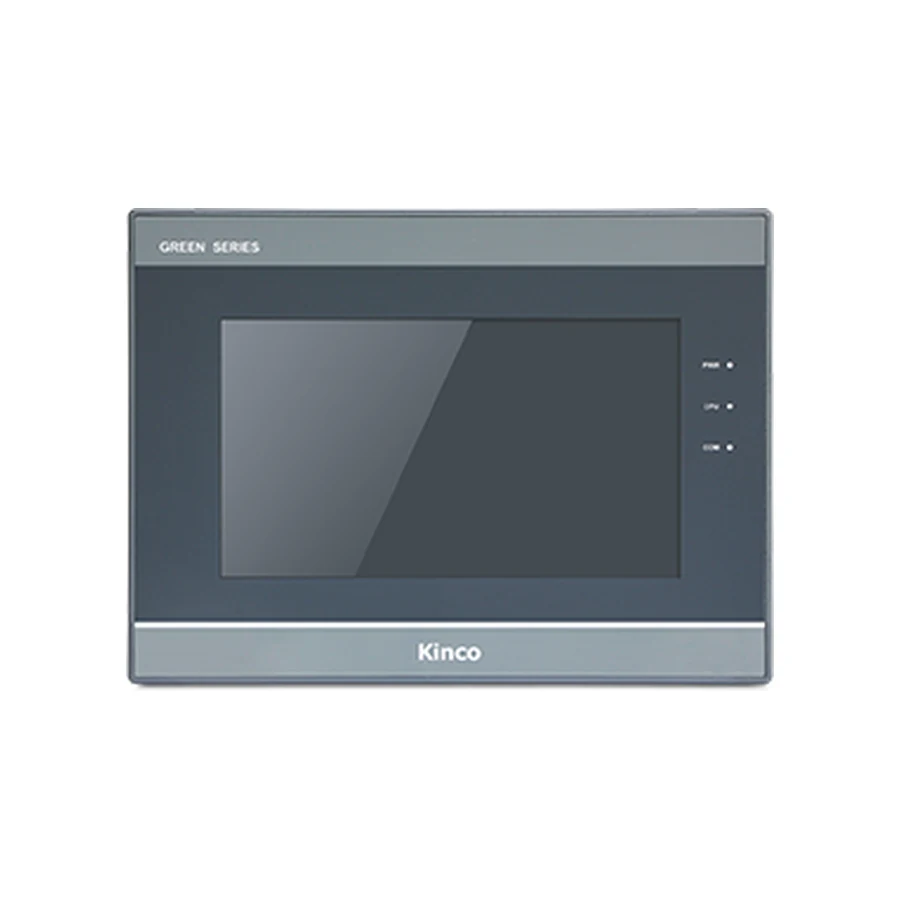
The Kinco G100 and G100E offer a 10.1-inch 1024 × 600 display with a 299 × 219 mm cut-out. This combination deserves attention when reviewing an existing DTools machine because screen diagonal alone will not identify the opening. G100E adds one Ethernet port, while both retain the listed serial set. Compare the 310 × 230 × 55 mm body, old project target and cable connections before choosing the full code for a larger operator view.
Kinco G100 HMI Panel Overview
G100 and G100E provide two connection choices within a shared G1 screen and cabinet format. The useful first question is whether the machine requires only its documented serial connection or also an Ethernet connection. Record that requirement beside the model rather than leaving purchasing to interpret the final letter.
The widescreen pixel area can accommodate related machine values and controls on one page, provided the application is designed for it. Review the normal operating page alongside the busiest alarm or setup page. A larger diagonal does not automatically improve usability if the same space is filled with smaller labels, crowded numeric fields or navigation that hides the operator’s next action.
G100 for Existing Cabinets with Larger Openings
The 299 × 219 mm opening is a defining selection point for this family. It deserves attention on an existing machine where the door has already been cut and changing metalwork would affect the scope of the job. Obtain an actual opening measurement instead of estimating it from a front photograph.
If a drawing merely says 10.1-inch HMI, identify the installed code before making a shortlist. The GL100 product family is another comparison route, but its listed 260 × 179 mm opening differs from the G100 opening. Screen diagonal therefore cannot serve as the mechanical requirement. In a new cabinet, assess available door space, operator reach and internal cable routing together before fixing the panel position.
G100 and G100E Ethernet and Serial-Port Hardware
G100 is the serial base selection. G100E adds an Ethernet port and the EdgeAccess 1.0 remote platform; Ethernet is not offered on the base G100. Neither code should be ordered on the assumption that a Wi-Fi or cellular function is included. Remote access also needs the applicable platform arrangement and site approval.
The display uses 4-wire resistive touch, with 128 MB RAM and 256 MB flash listed for both codes. These values belong in the project-capacity review, especially when the old application has accumulated graphics, recipes or stored history. Plan actual retention and export requirements within the application design. The product’s existing specification and code comparison tables remain the place to inspect the complete hardware values.
G100 PLC Ports and Driver Checks
Both codes list COM0 as RS232/RS485/RS422, COM1 as RS485/RS422 and COM2 as RS232. Document which logical port the working project uses and which pins the machine cable actually connects. Matching connector shapes are insufficient when the electrical mode or signal assignment differs.
Match G100 PLC Drivers and Cable Pinout
For G100E Ethernet communication, identify the PLC CPU, module, firmware and required protocol before choosing a DTools driver. For serial communication, add the station settings and wiring diagram. The PLC compatibility guide helps organize these checks; the PLC no-response diagnostic process addresses failures after the intended connection has been documented.
Agree on read-only commissioning values first. Where a write test is necessary, use a safely stopped machine or isolated test setup with the responsible PLC engineer. Validate the requested action through the PLC’s normal permissions and interlocks.
G100 299 × 219 mm Cut-out and Body Dimensions
Measure the 299 × 219 mm Opening for G100
The body measures 310 × 230 × 55 mm, separately from the 299 × 219 mm cut-out. Inspect the door around the opening for obstructions, available clamp positions and enough front clearance. At the rear, include the connectors and their cable bend radius when assessing the 55 mm body depth.
An existing enclosure may have a duct or terminal rail directly behind the screen. Photograph that area and measure with the door in its working position, because a static front view misses the interference. Use a code-applicable installation drawing for machining and mounting details; product images and the illustrative cut-out diagram cannot establish a pinout. The listed supply input is DC 12 to 28 V. Review the actual cabinet supply, polarity and grounding before installation.
Kinco DTools is listed for G100 and G100E. Archive the editable project and record the release that produced the working machine application. Open a separate copy for target and driver review, keeping the running system’s settings available for comparison.
The DTools software for G100 article explains the general acquisition and version process. Request a G100 or G100E manual by full code and hardware revision where relevant. During project review, inspect screen size, fonts, alarm text, recipe handling and every PLC connection. Pay particular attention when the project file came from a similar panel: the software family name does not prove that its target, communication settings or retained data match this machine.
G100 Existing-Panel Fit and Project Checks
The Kinco GH104E HMI Panel provides a useful existing-cabinet comparison: its listed opening is also 299 × 219 mm, but the display resolution is 800 × 600 rather than G100’s 1024 × 600. Both list DTools. That difference affects page proportions and object placement even when the opening matches.
The G2100E DTools Pro family offers another selection direction when evaluating a different hardware and software generation. Compare its own dimensions and connection options rather than transferring G100 assumptions. For the broader process, follow the G100 project migration checks and HMI panel replacement checklist. Keep this decision focused on fit, target and connection evidence before scheduling application conversion.
G100 Price and Quotation Details
A useful G100 inquiry identifies the actual order as G100 or G100E. Add quantity, destination and the requested delivery date. If the cabinet opening is driving the selection, state the measured dimensions and whether the rear installation space can change. These details allow the quotation to address a specific requirement.
For a maintenance purchase, include the installed nameplate and project version. For an engineering review, add PLC identification and the proposed serial or Ethernet connection. Request the relevant datasheet, manual or installation drawing with the document language specified. Pricing and lead time depend on the individual inquiry; a generic request for a 10-inch screen leaves both the cabinet and the network choice unresolved.
G100 Selection FAQ
How do G100, G100E differ?
G100E adds Ethernet and EdgeAccess 1.0. Both share the listed screen, memory and serial-port set. Select using the required connection rather than expecting an Ethernet cable to work with the serial base.
What cut-out and rear clearance does G100 need?
The opening is 299 × 219 mm and the body is 310 × 230 × 55 mm. Add connector, wire-bend and service space using the applicable installation drawing.
How do I check G100 against my PLC driver and project?
Match the controller and protocol to the DTools driver, inspect the project target and verify the cable. Plan controlled application tests before returning a changed panel to machine operation.
How can I request a G100 datasheet, manual or quotation?
Send G100 or G100E, any relevant revision and the document language. Add quantity and destination for pricing, plus the old panel details when assistance with selection is required.
Comprehensive Field Maintenance and Operational Sign-Off
Ensuring long-term operational dependability on industrial equipment demands establishing structured routine inspection routines and preventative maintenance standards across all production shifts. Maintenance personnel should regularly verify that enclosure door hinges and structural latches retain sufficient mechanical tension to preserve continuous sealing pressure across the front bezel perimeter gasket. In manufacturing environments exposed to continuous mechanical vibration from heavy punch presses or stamping tools, technicians should periodically inspect rear screw terminal blocks and cable restraint clamps to prevent loose electrical terminations.
Before returning modified machinery to active production service, engineering teams should execute a formal commissioning sign-off protocol. Verify that emergency stop interlocks function independently of terminal software screens, confirm that communication retry counters operate within acceptable thresholds under peak network loading, and archive both the active PLC runtime image and the compiled operator interface project files into the central engineering repository.